Steam Condensate Recovery Systems for Energy & Water Efficiency

Steam Condensate Recovery Systems for Energy & Water Efficiency

Engineered to recover and reuse condensate from steam systems, improving thermal efficiency, reducing water consumption, and minimizing operational energy losses across industrial processes.

Recovers heat and water from steam condensate
Reduces boiler fuel and water consumption
Improves overall steam system efficiency
Industrial energy solution

| About

What are Steam Condensate Recovery Systems?

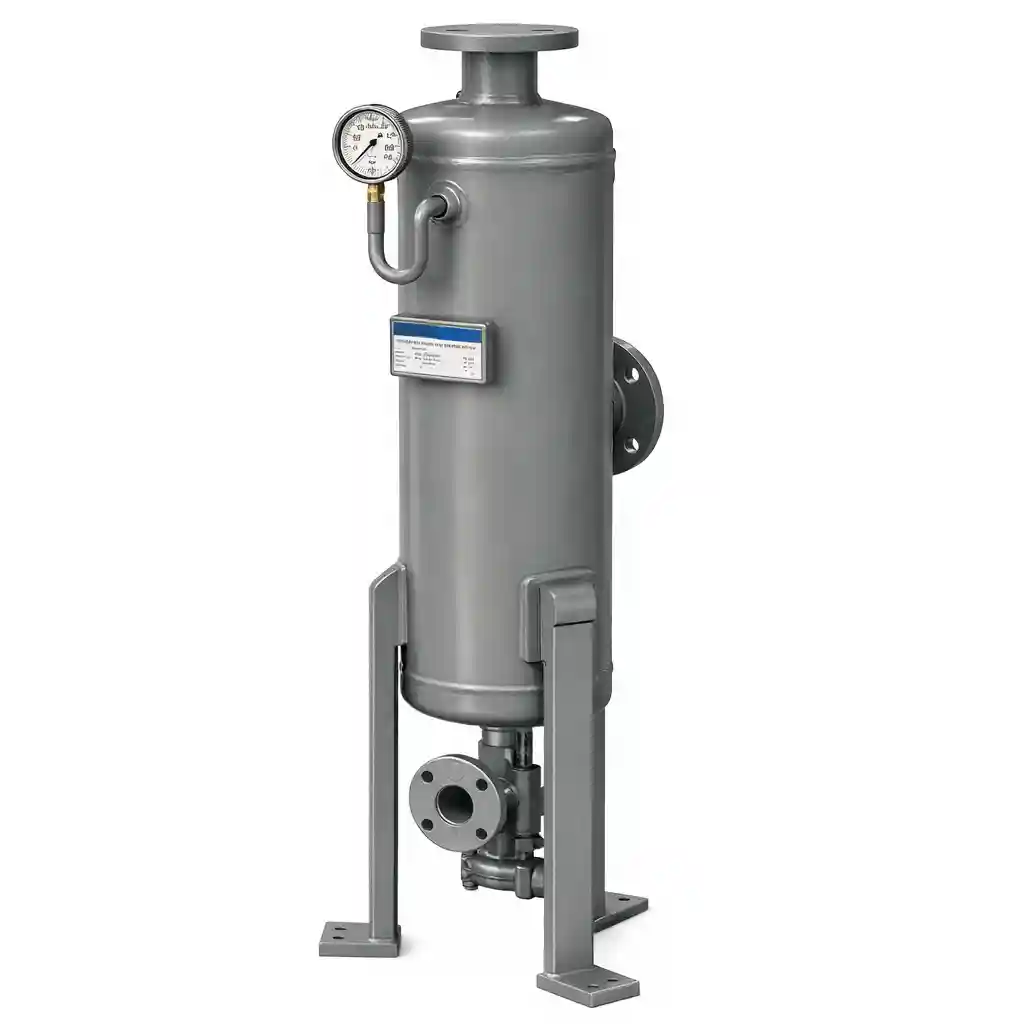
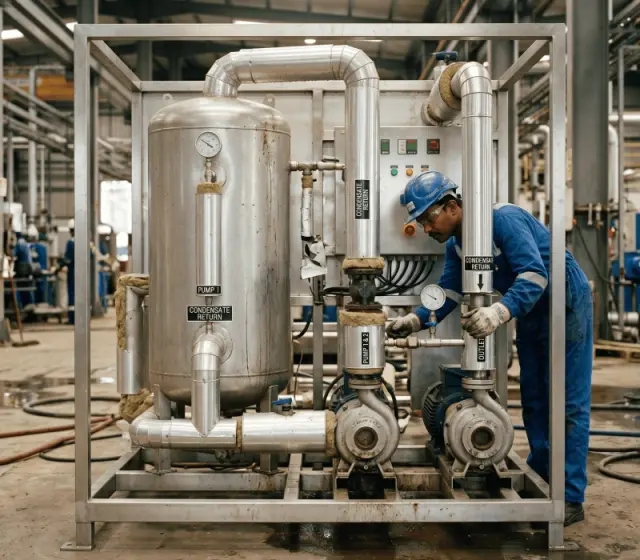
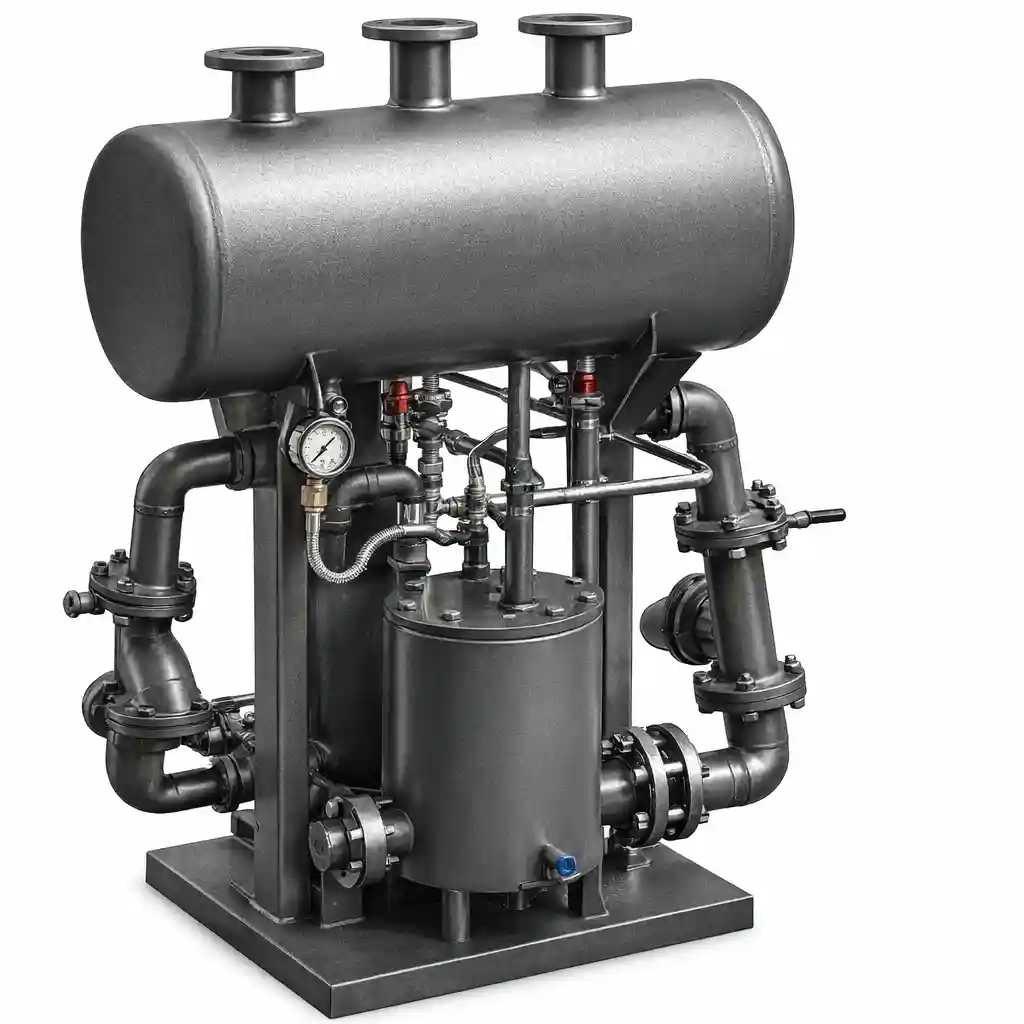
Steam condensate recovery systems are industrial utility systems designed to collect, recover, and reuse condensate generated from steam-based heating and process applications.

Instead of discarding hot condensate, these systems return it back to the boiler or process loop, conserving both heat energy and treated water. Condensate recovery plays a critical role in improving steam system efficiency, lowering operational costs, and reducing energy and water wastage across industrial facilities.

What are Steam Condensate Recovery Systems?

| Process

How It Works

01

Steam Heat Transfer

Steam transfers heat during industrial processes and condenses into hot water

02

Condensate Collection

Condensate is collected through piping and recovery systems

03

Condensate Transfer

Recovery pumps or pressure systems transfer condensate back to the boiler feed system

04

Boiler Heat Reduction

Recovered hot water reduces boiler heating requirements

05

Water Reuse

Reused condensate minimizes fresh water and chemical treatment demand

| Industries

Applications

Ideal for steam-based industrial utility optimization

Industrial Steam & Boiler Systems

Steam utility efficiency and heat recovery

Textile & Food Processing

Steam condensate reuse for thermal efficiency

Chemical & Pharmaceutical Plants

Process heating utility optimization

Power Generation Systems

Condensate recycling for thermal performance

Manufacturing Facilities

Steam-based process energy recovery

| Advantages

Key Benefits

| Specifications

Key Features

Engineered for efficient condensate recovery and utility optimization

Automated Condensate Collection

Continuous condensate capture and transfer

High-Temperature Components

Industrial-grade piping and recovery systems

Integrated Pumps & Pressure Systems

Reliable condensate return mechanisms

Corrosion-Resistant Construction

Long operational durability

Energy-Efficient Recovery Design

Optimized thermal and water conservation

Monitoring & Control Systems

Operational visibility and automation

Steam Infrastructure Compatibility

Works with existing industrial systems

Custom Plant Configurations

Tailored to plant-specific requirements

| Comparison

Why Choose This Technology?

Over Conventional Steam Systems

  • Prevents wastage of heat and treated water
  • Improves overall steam system performance significantly

Over Manual Recovery Methods

  • Automated and efficient condensate management
  • Better operational reliability and monitoring capability

Long-Term Advantage

  • Long-term reduction in utility and operational costs
  • Supports energy conservation and sustainability goals

| Sector Focus

Industry-Specific Applications

Textile Industry

Steam condensate reuse in dyeing and processing operations

Food Industry

Heat recovery from steam-based production systems

Chemical Industry

Utility optimization for process heating systems

Power Plants

Condensate recycling for improved thermal efficiency

| Gallery

Steam Condensate Recovery Systems in Action

Industrial steam efficiency, condensate reuse, and utility optimization systems

Want to Improve Steam System Efficiency?

Get a customized condensate recovery solution for your plant
Speak with our engineering experts for utility optimization planning
Request detailed specifications and consultation