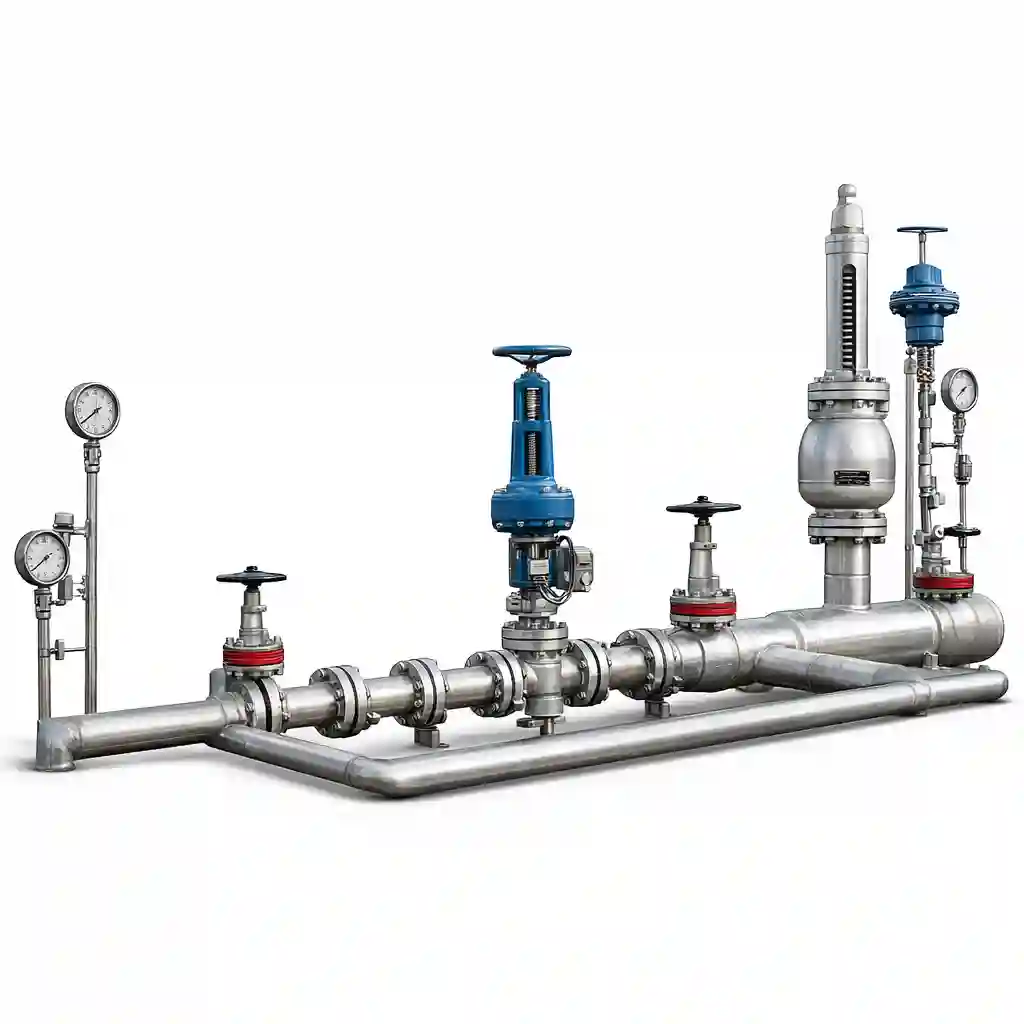
Industrial Valves for Precise Flow & Pressure Control

Industrial Valves for Precise Flow & Pressure Control

Engineered for reliable fluid regulation, pressure management, and process control across industrial piping and utility systems under demanding operating conditions.

Accurate flow and pressure control across industrial systems
Designed for high-temperature and high-pressure applications
Suitable for water, steam, gas, and process fluid handling
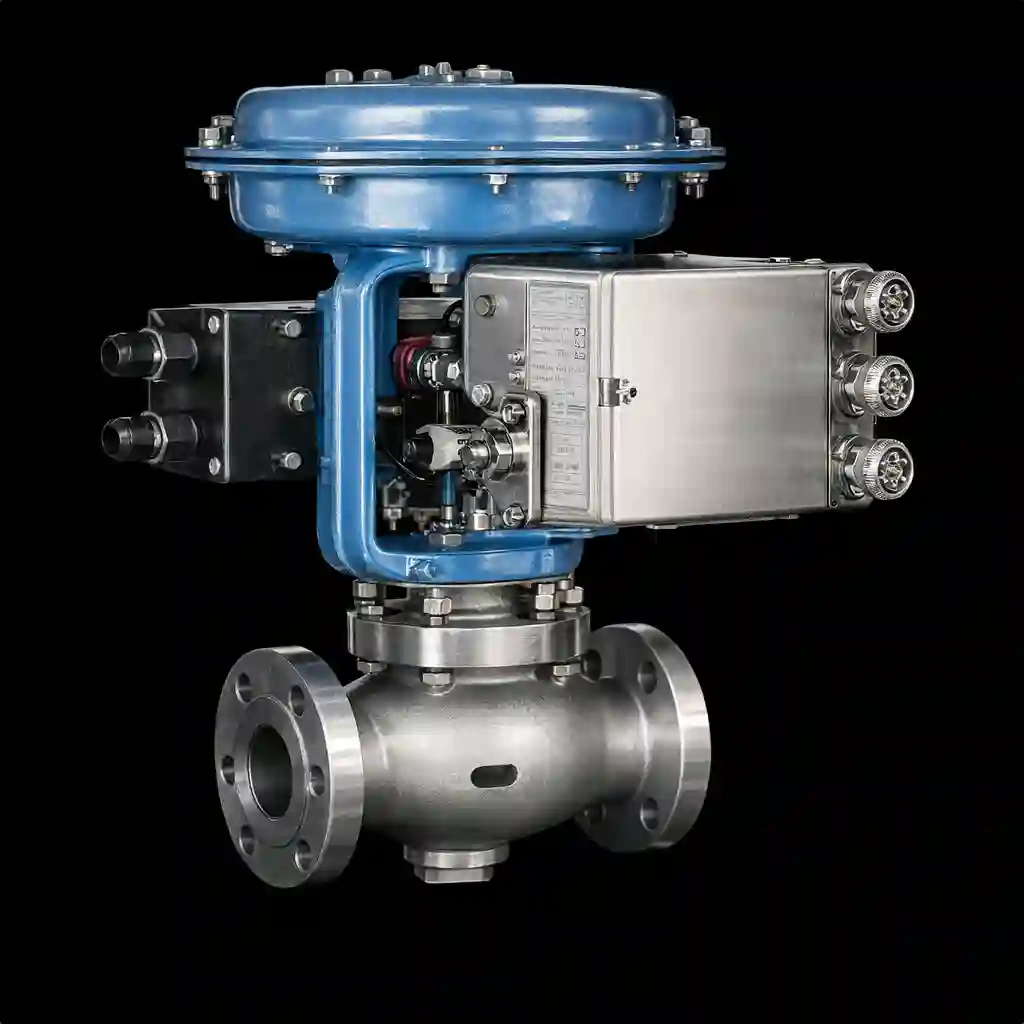
Industrial energy solution

| About

What are Industrial Valves?

Industrial valves are mechanical flow control devices designed to regulate, isolate, direct, or control the flow of liquids, gases, steam, and process fluids within industrial systems.

These valves are critical components across pipelines, utility networks, and process plants requiring operational control and safety management. Different valve types such as gate valves, globe valves, butterfly valves, ball valves, and control valves are selected based on pressure, temperature, fluid type, and operational requirements.

What are Industrial Valves?

| Process

How It Works

01

Valve Operation Mechanism

Valves operate through manual, pneumatic, hydraulic, or automated mechanisms

02

Flow Regulation

Internal valve components regulate fluid flow or pressure within pipelines

03

Control Actions

Opening, closing, or throttling actions control process conditions

04

Leak Prevention

Sealing systems ensure leak prevention and operational safety

05

Automated Process Control

Automated control systems can regulate valves based on process parameters

| Industries

Applications

Ideal for industrial flow, pressure, and process control systems

Industrial Steam & Utility Systems

Steam, gas, and utility pipeline control

Water & Wastewater Plants

Water flow and treatment process management

Chemical & Process Industries

Fluid and gas regulation systems

Oil, Gas & Power Systems

Pressure and operational control applications

Manufacturing & Infrastructure

Industrial process and utility flow systems

| Advantages

Key Benefits

| Specifications

Key Features

Engineered for durable and precise industrial flow management

Heavy-Duty Valve Construction

Industrial durability for demanding operations

Multiple Valve Configurations

Gate, globe, check, and control valve options

High-Performance Sealing

Leak prevention and operational safety

Actuator Compatibility

Automation-ready process control integration

Corrosion-Resistant Materials

Long-term operational durability

High-Temperature & Pressure Design

Industrial-grade process compatibility

Smooth Flow Regulation

Optimized operational precision

Custom Engineered Solutions

Tailored to application-specific industrial requirements

| Comparison

Why Choose This Technology?

Over Basic Flow Control Systems

  • Improved operational accuracy and process safety
  • Higher durability for industrial operating environments

Over Conventional Manual Systems

  • Automation-ready configurations for process optimization
  • Better pressure and flow regulation capability

Long-Term Advantage

  • Reduced operational losses and maintenance requirements
  • Reliable long-term process control solution

| Sector Focus

Industry-Specific Applications

Power Plants

Steam and pressure regulation systems

Chemical Industry

Process fluid and gas control applications

Water Treatment

Water flow and distribution systems

Manufacturing Industry

Utility and process pipeline control

| Gallery

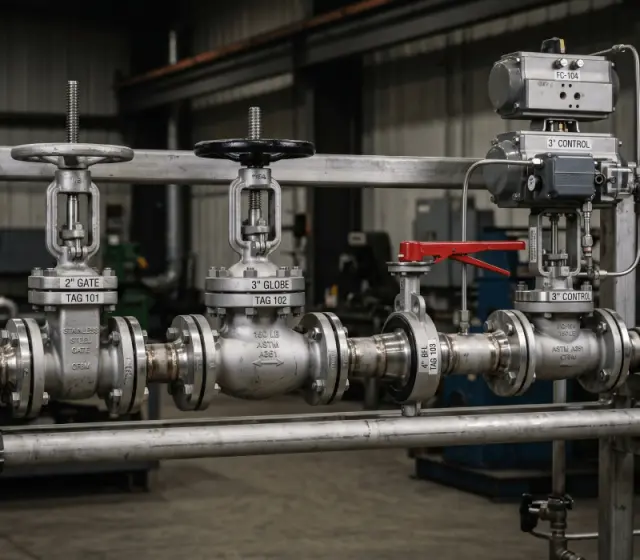
Industrial Valve Systems in Action

Industrial flow control, pressure management, and automated valve systems

Looking for Reliable Industrial Valve Solutions?

Get a customized valve solution for your operations
Speak with our engineering experts for system selection and application support
Request detailed technical specifications and consultation